


Liquid Cooling Connectors
Liquid cooling connectors are precision-engineered stainless steel tube and fitting assemblies purpose-built for server liquid cooling, CDU systems, immersion cooling, and energy storage thermal management. Manufactured from 304/316L stainless steel to ASTM A312 and JIS G3459, with internal...
Product Introduction
Liquid cooling connectors are precision-engineered stainless steel tube and fitting assemblies purpose-built for server liquid cooling, CDU systems, immersion cooling, and energy storage thermal management.
Manufactured from 304/316L stainless steel to ASTM A312 and JIS G3459, with internal surface roughness down to Ra ≤0.4 μm and 100% leak inspection before shipment. China Super Tech has produced these assemblies since 2013 - 12,000 tons annual capacity, exports to 20+ countries, 600+ customer projects delivered.
A manufacturer engineer replies within 24 hours.

What Goes Wrong in Liquid Cooling Projects
Liquid cooling connectors fail in ways that standard industrial tubing never does. Each of these failure modes carries a specific installation, uptime, or supply-chain cost.
Leak at a Weld Joint
A coolant leak at a weld joint forces emergency rack shutdown - one connector, 12 hours of lost uptime, and a thermal event risk to every adjacent server.
Drawing Interpretation Errors
Custom connector drawings get misread by suppliers without liquid cooling experience - wrong interface angle, off-by-2 mm dimension, entire batch rejected at installation.
Batch-to-Batch Dimensional Drift
Batch-to-batch dimensional drift, typically outside ±0.1 mm, makes the second delivery incompatible with the first - on-site assembly slows to a crawl while technicians re-fit each joint.
Slow Supplier Response
Supplier response lags 3-5 days on feasibility and lead time, freezing CDU connection work on the critical path.

Connector Design for High-Density Cooling Systems
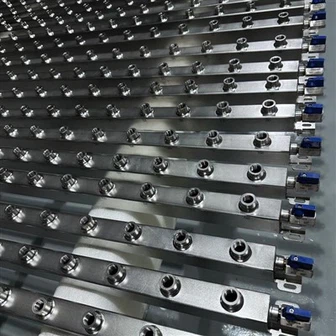
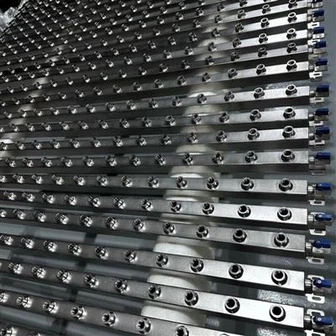
Liquid cooling connectors are used where standard straight tubing is not enough: tight rack layouts, CDU connections, manifold branches, custom interfaces, and pre-assembled cooling loops.
For projects requiring integrated coolant distribution, see our Data Center Liquid Cooling Manifold Pipe and Server Liquid Cooling Manifold solutions.
The objective is not simply to produce a connector. The objective is to maintain dimensional fit, weld integrity, internal cleanliness, and leak performance from the first batch through volume production.
Differentiation and Competitive Comparison
The following comparison focuses on the manufacturing and quality-control dimensions that directly affect liquid cooling installation and operation.
| Dimension | This Product | Industry Conventional | Differential Value |
|---|---|---|---|
| Internal surface roughness | Ra ≤0.4 μm, verified per surface-finish standard | Ra ≤0.8-1.6 μm typical | Reduces particle accumulation; extends coolant replacement cycle |
| Welding quality control | ISO 3834-certified, orbital welding + 100% leak inspection | Visual weld inspection, spot leak test | Detection limit 1×10⁻⁹ Pa·m³/s; near-zero weld-failure risk |
| Batch consistency | ±0.1 mm dimensional tolerance held across every batch | ±0.2-0.3 mm common batch drift | Direct-assembly fit; no re-work on site |
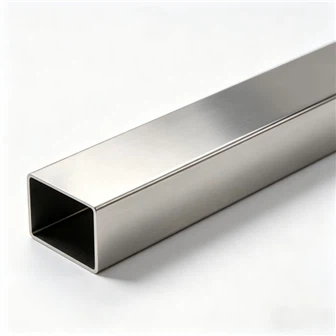
| Customization range | Square tubes 10×10 to 80×80 mm; wall 0.5-3.0 mm; length to 6000 mm | Standard straight tubes only | Complex layouts integrated without extra fabrication steps |
| Material control | 304/316L with molybdenum for chloride/pitting resistance; full chemical composition inspection per batch | Grade stated on cert only | Stable corrosion performance in glycol-based coolants |
| 5-year TCO | Lower total cost from reduced leak-rework and coolant maintenance | Higher total cost from re-work and coolant replacement | 30% lower total cost over 5 years |
Three Process Controls Behind Connector Consistency
The numbers above hold because manufacturing is controlled end-to-end. Three process facts do the heavy lifting.
Material Verification & Grade Control
Each 304/316L batch is checked by spectrometer for chemical composition against ASTM A312, so chromium and molybdenum content stays inside spec batch after batch.
Orbital Welding with ISO 3834 Management
Weld penetration is set by machine parameters, not operator feel, removing the human variable that causes most liquid cooling failures.
Internal Surface Optimization
Polishing, pickling, and passivation bring roughness down to Ra ≤0.4 μm, which keeps particle counts low and protects coolant pumps downstream.
Integrated Manufacturing and Inspection
Key components are specified, not sourced on price: the orbital welding heads run with controlled arc parameters certified under ISO 3834; passivation chemistry is validated against ASTM A967; leak-test equipment is calibrated to a 1×10⁻⁹ Pa·m³/s detection limit.
Every connector passes seven inspection gates:
- Incoming inspection - chemical composition per ASTM A312.
- In-process dimensional check - outer diameter, wall thickness measured to ±0.1 mm.
- Weld inspection - visual + dye penetrant per ISO 3834 criteria.
- Surface verification - roughness meter reading against Ra ≤0.4 μm target.
- 100% leak test - helium pressure decay, acceptance at 1×10⁻⁹ Pa·m³/s.
- Final shipment approval - batch traceability number issued.
- Third-party verification - SGS / TÜV / BV reports available on request.

Seven Inspection Gates Before Shipment
Technical Specifications
304 and 316L stainless steel options are available according to coolant chemistry, dimensions and operating environment.
Dimensional & Mechanical
| Square tube outer size | 10×10 to 80×80 mm |
| Wall thickness | 0.5-3.0 mm |
| Length | Up to 6000 mm |
| Tensile strength | ≥515 MPa |
| Yield strength | ≥205 MPa |
| Standard | ASTM A312 |
Chemical & Surface
| 316L Chromium | 16.0-18.0% |
| 316L Molybdenum | 2.0-3.0% |
| 316L Carbon | ≤0.030% |
| Internal roughness | Ra ≤0.4 μm |
| Helium leak rate | ≤1×10⁻⁹ Pa·m³/s |
| Standards | ASTM A312 / JIS G3459 |
316L selection logic: 316L is the default for glycol-based and chloride-exposed loops because molybdenum and low carbon push pitting resistance higher than 304 - the parameter matters because coolant chemistry stays aggressive for the life of the rack.
304 remains the economical pick for pure-water and DI-water loops.
For projects where the primary decision is 304 vs 316L, see our 316 vs 304 Liquid Cooling Manifolds: Material Selection Guide.
Technical Customization
Custom connectors can be produced according to drawings, dimensions, bend requirements and system interfaces.
| Custom Dimension | Range / Options | Verification |
|---|---|---|
| Tube geometry | Square 10×10 to 80×80 mm; round custom | Dimensional inspection per drawing |
| Bending | Custom bend angles, radii | Bend-template gauge check |
| Manifolds | Custom port count and layout | Dye penetrant + leak test |
| Assemblies | Welded connector + tube integration | 100% leak inspection |
| Surface finish | Ra ≤0.4 μm to Ra ≤0.8 μm (specified) | Roughness meter report |
| Length | Cut-to-length up to 6000 mm | Tape measure against drawing |
01 · Drawing Review
Requirement confirmation and drawing review within 24 hours.
02 · Solution Design
Connector geometry, interface and manufacturing feasibility are confirmed before production.
03 · Prototype
Prototype custom connectors can be produced for project validation.
04 · Mass Production
Production scheduling supports standard and customized orders in parallel.
05 · QC
Dimensional, surface, welding and leak inspections are completed before shipment.
06 · Delivery
Export-grade packaging and batch traceability support project installation.
For larger manifold configurations, see our Stainless Steel Square Manifold and 316 Liquid Cooling Manifolds.
Applications
Connector configurations are selected according to the coolant, installation space, operating temperature and system architecture.
AI Data Centers
Rack-level liquid cooling loops. Recommended: 316L, Ra ≤0.4 μm. Glycol-water, 45-65°C.
CDU Systems
Coolant distribution unit manifolds. 316L manifolds + assemblies. Sealed loop, 3-6 bar.
Immersion Cooling
Tank piping and connector joints. 316L welded assemblies. Dielectric fluid, 40-55°C.
Energy Storage
BESS thermal management loops. 304 or 316L. Glycol-water, sealed.
Power Electronics
IGBT and inverter cooling. 304, straight and bent tubes. DI-water, ≤80°C.
Designed Around the Actual Cooling Loop
Connector geometry can be adapted to rack-level liquid cooling, CDU distribution, immersion cooling tanks, energy storage loops and power electronics cooling.
For immersion applications, see our Immersion Cooling System page for additional tube, manifold and welded assembly information.
Customer Cases
Project examples showing how dimensional consistency, customized geometry and prefabricated assemblies affect installation efficiency.
A data center infrastructure team in Singapore retrofitted an existing rack design with only 180 mm of installation clearance - customized bent 316L connectors reduced assembly time from 4 hours to 70 minutes per rack.
A CDU system integrator in Germany has taken 8 consecutive deliveries of orbital-welded manifolds since 2022 - incoming dimensional reports show zero out-of-tolerance parts across 6,400 units.
An energy storage manufacturer in Texas runs 316L connectors in glycol loops at 55°C, 24/7, since 2023 - zero leak incidents across 18 months of continuous operation.
An Indian power electronics maker converted from a cheap 304 supplier whose second batch drifted 0.35 mm - after switching, their IGBT cooling assembly line scrap rate fell from 4.2% to under 0.4%.
Why Batch Consistency Comes First
Every batch matches the first because the process is locked, not the operator. A pre-shipment pressure test and helium leak test on 100% of units catches what sample checks miss.
Chemical composition verification on incoming material catches material substitution before it enters production.
When a liquid cooling connector arrives, it fits - and it keeps fitting on delivery #30 the same as delivery #1.
Frequently Asked Questions
Expand each question to review the technical and procurement details.
Key Takeaways
Order, Delivery, and Support
After-Sales Service
| Warranty | 24 months from shipment, covering weld and dimensional manufacturing defects. |
| Technical response | Within 24 hours. |
| On-site support | Arranged with local partners where available. |
| Spare parts | Dispatched from bonded inventory within 48 hours. |
| Support channels | WhatsApp, email, online chat, phone. |
Logistics & Delivery
| Annual capacity | 12,000 tons - enough to outfit roughly 30,000 standard AI racks per year. |
| Standard lead time | 10-15 days. |
| Prototype | 7 days. |
| Custom production | 20-30 days. |
| Packaging | Export-grade wooden crate with anti-corrosion wrapping and end-cap protection. |
| Samples | Free samples available on request; sample delivery in 7-10 days. |
Request a Quote for Liquid Cooling Connectors
Send your connector dimensions, material requirements and quantity. The engineering team can review the project requirements and respond within 24 hours.
Company name
Product requirements - size, material, quantity, application
Response commitment: a manufacturer engineer replies within 24 hours.
Hot Tags: liquid cooling connectors, China liquid cooling connectors manufacturers, suppliers, factory
You Might Also Like


Send Inquiry
