
Precision Liquid Cooling Manifolds for High-Density Thermal Management
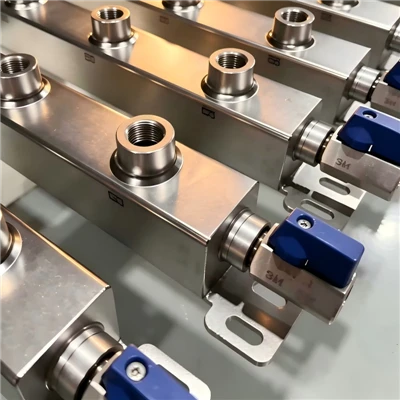
Engineered for high-performance computing, data center server racks, and industrial power electronics, our liquid cooling manifolds provide balanced fluid distribution and collection across multi-channel thermal loops. Built from corrosion-resistant alloy profiles and precision CNC-machined blocks, these distribution headers maintain low pressure drops and absolute leak-tight integrity under continuous operating pressures up to 16 bar. We support custom port layouts, integrated flow controls, and strict metallurgical traceability for OEM thermal system integrators.


Product Types
Block-Type CNC Machined Manifolds:
Solid bar stock milled from 316L stainless steel or 6061-T6 aluminum, eliminating internal brazed joints to maximize structural reliability under vibration and thermal cycling.
Tubular Header Assemblies:
Precision-drawn primary trunk tubes featuring branch ports TIG-welded or silver-brazed with controlled penetration to prevent internal restriction or turbulence.
Custom Multi-Port Distribution Manifolds:
Configured with mixed port sizes (e.g., 1-inch main inlet transitioning to multiple 1/4-inch or 3/8-inch branch outlets) matching specific rack or cold plate layouts.
Valved & Quick-Disconnect Integrated Manifolds:
Assemblies pre-equipped with ball valves, flow meters, or leak-free quick-disconnect sockets for modular maintenance.
Technical Specifications
| Parameter | Standard Specification Range | Customization Capability |
| Main Trunk Diameter | DN15 to DN100 (1/2 inch to 4 inches) | Up to DN150 based on flow requirements |
| Branch Port Configuration | 2 to 32 ports per assembly | Custom spacing, staggered or inline layout |
| Thread Standards | NPT, BSPP (G-thread), SAE, Metric (ISO 6149) | Flanged, sanitary tri-clamp, or stub-end connections |
| Maximum Working Pressure | Up to 1.6 MPa (16 bar / 232 psi) | High-pressure ratings up to 2.5 MPa upon request |
| Operating Temperature Range | -20°C to +120°C | Extended range up to +150°C with high-temp seals |
| Internal Surface Finish | Ra ≤ 0.8 μm (Standard as-machined/passivated) | Electropolished to Ra ≤ 0.4 μm |
Materials & Surface Finish
Materials:
316L / 304 Stainless Steel (chloride pitting resistance), Aluminum Alloy 6061-T6 (lightweight thermal modules), C11000 Copper, and Cupronickel (C70600) for specialized marine or chemical coolant compatibility.
Surface Passivation:
Stainless steel components undergo chemical passivation in accordance with ASTM A967 to eliminate free iron and maximize surface chromium oxide protective layers.
Anodizing:
Aluminum manifolds receive MIL-A-8625 Type III hardcoat anodizing or clear chromate conversion coating to prevent oxidation and galvanic interaction in mixed-metal coolant loops.
Cleaning:
Ultrasonic degreasing and particle flushing to ensure internal cleanliness, eliminating manufacturing debris prior to final sealing and shipment.
Performance Features
Equalized Flow Distribution:
Sized trunk geometries and optimized port transition angles minimize flow maldistribution across parallel cooling channels, ensuring uniform thermal transfer.
01
Low Pressure Drop:
Smooth internal transitions and absence of weld root sag reduce hydraulic resistance, lowering pump energy consumption in closed-loop systems.
02
Zero-Leakage Integrity:
Eliminated porosity through solid billet machining and rigorous joint testing prevents coolant weeping or catastrophic dielectric fluid loss.
03
Galvanic Corrosion Mitigation:
Material pairing guidelines and isolation accessories prevent electrochemical degradation when combining copper cold plates, aluminum panels, and stainless headers.
04
Data Center Cooling Distribution Units (CDUs): Primary and secondary fluid routing headers for server rack liquid loops.
AI Server & GPU Cooling: Direct-to-chip thermal management modules handling high heat flux dissipation.
Power Electronics: Inverter and converter cooling in renewable energy wind and solar installations.
Medical Imaging Equipment: Laser diode and MRI gradient coil chiller circulation manifolds.
Selection Guide: Choose 316L stainless steel for deionized water and corrosive glycol mixtures where long-term passivation is critical. Select aluminum 6061 for weight-sensitive mobile or rack-mounted enclosures where closed-loop inhibited coolants are utilized.
Manufacturing & Quality Control
CNC Machining Centers:
Multi-axis vertical and horizontal CNC milling machines maintain positional hole tolerances within ±0.05 mm for precise alignment with mating hardware.
Welding & Brazing Qualification:
TIG welding operators certified to ASME Section IX standards; controlled atmosphere vacuum brazing ensures void-free filler penetration.
Pressure & Leak Testing:
100% pneumatic pressure testing under 1.5 times working pressure, supplemented by helium mass spectrometer leak detection for high-reliability vacuum or dielectric applications.
Dimensional Inspection:
CMM (Coordinate Measuring Machine) verification of port centerlines, thread depths, and geometric tolerances prior to batch release.
Custom Tube Manufacturing
Standard off-the-shelf manifolds frequently fail to accommodate restricted spatial envelopes inside server chassis or specialized industrial cabinets. We engineer custom liquid cooling manifolds directly from client 3D CAD models (STEP, IGES, SolidWorks). Capabilities include custom port positioning, integrated mounting brackets, specialized flange interfaces, and unique geometric profiling to fit tight enclosure constraints without compromising hydraulic performance.
Certifications


FAQ
As one of the most professional liquid cooling manifold manufacturers and suppliers in China, we're featured by quality products and good service. Please rest assured to wholesale OEM liquid cooling manifold from our factory. Also, custom service is available.
battery cooling manifold, high tolerance smooth tube, machined cooling manifold